







Real-world application reports
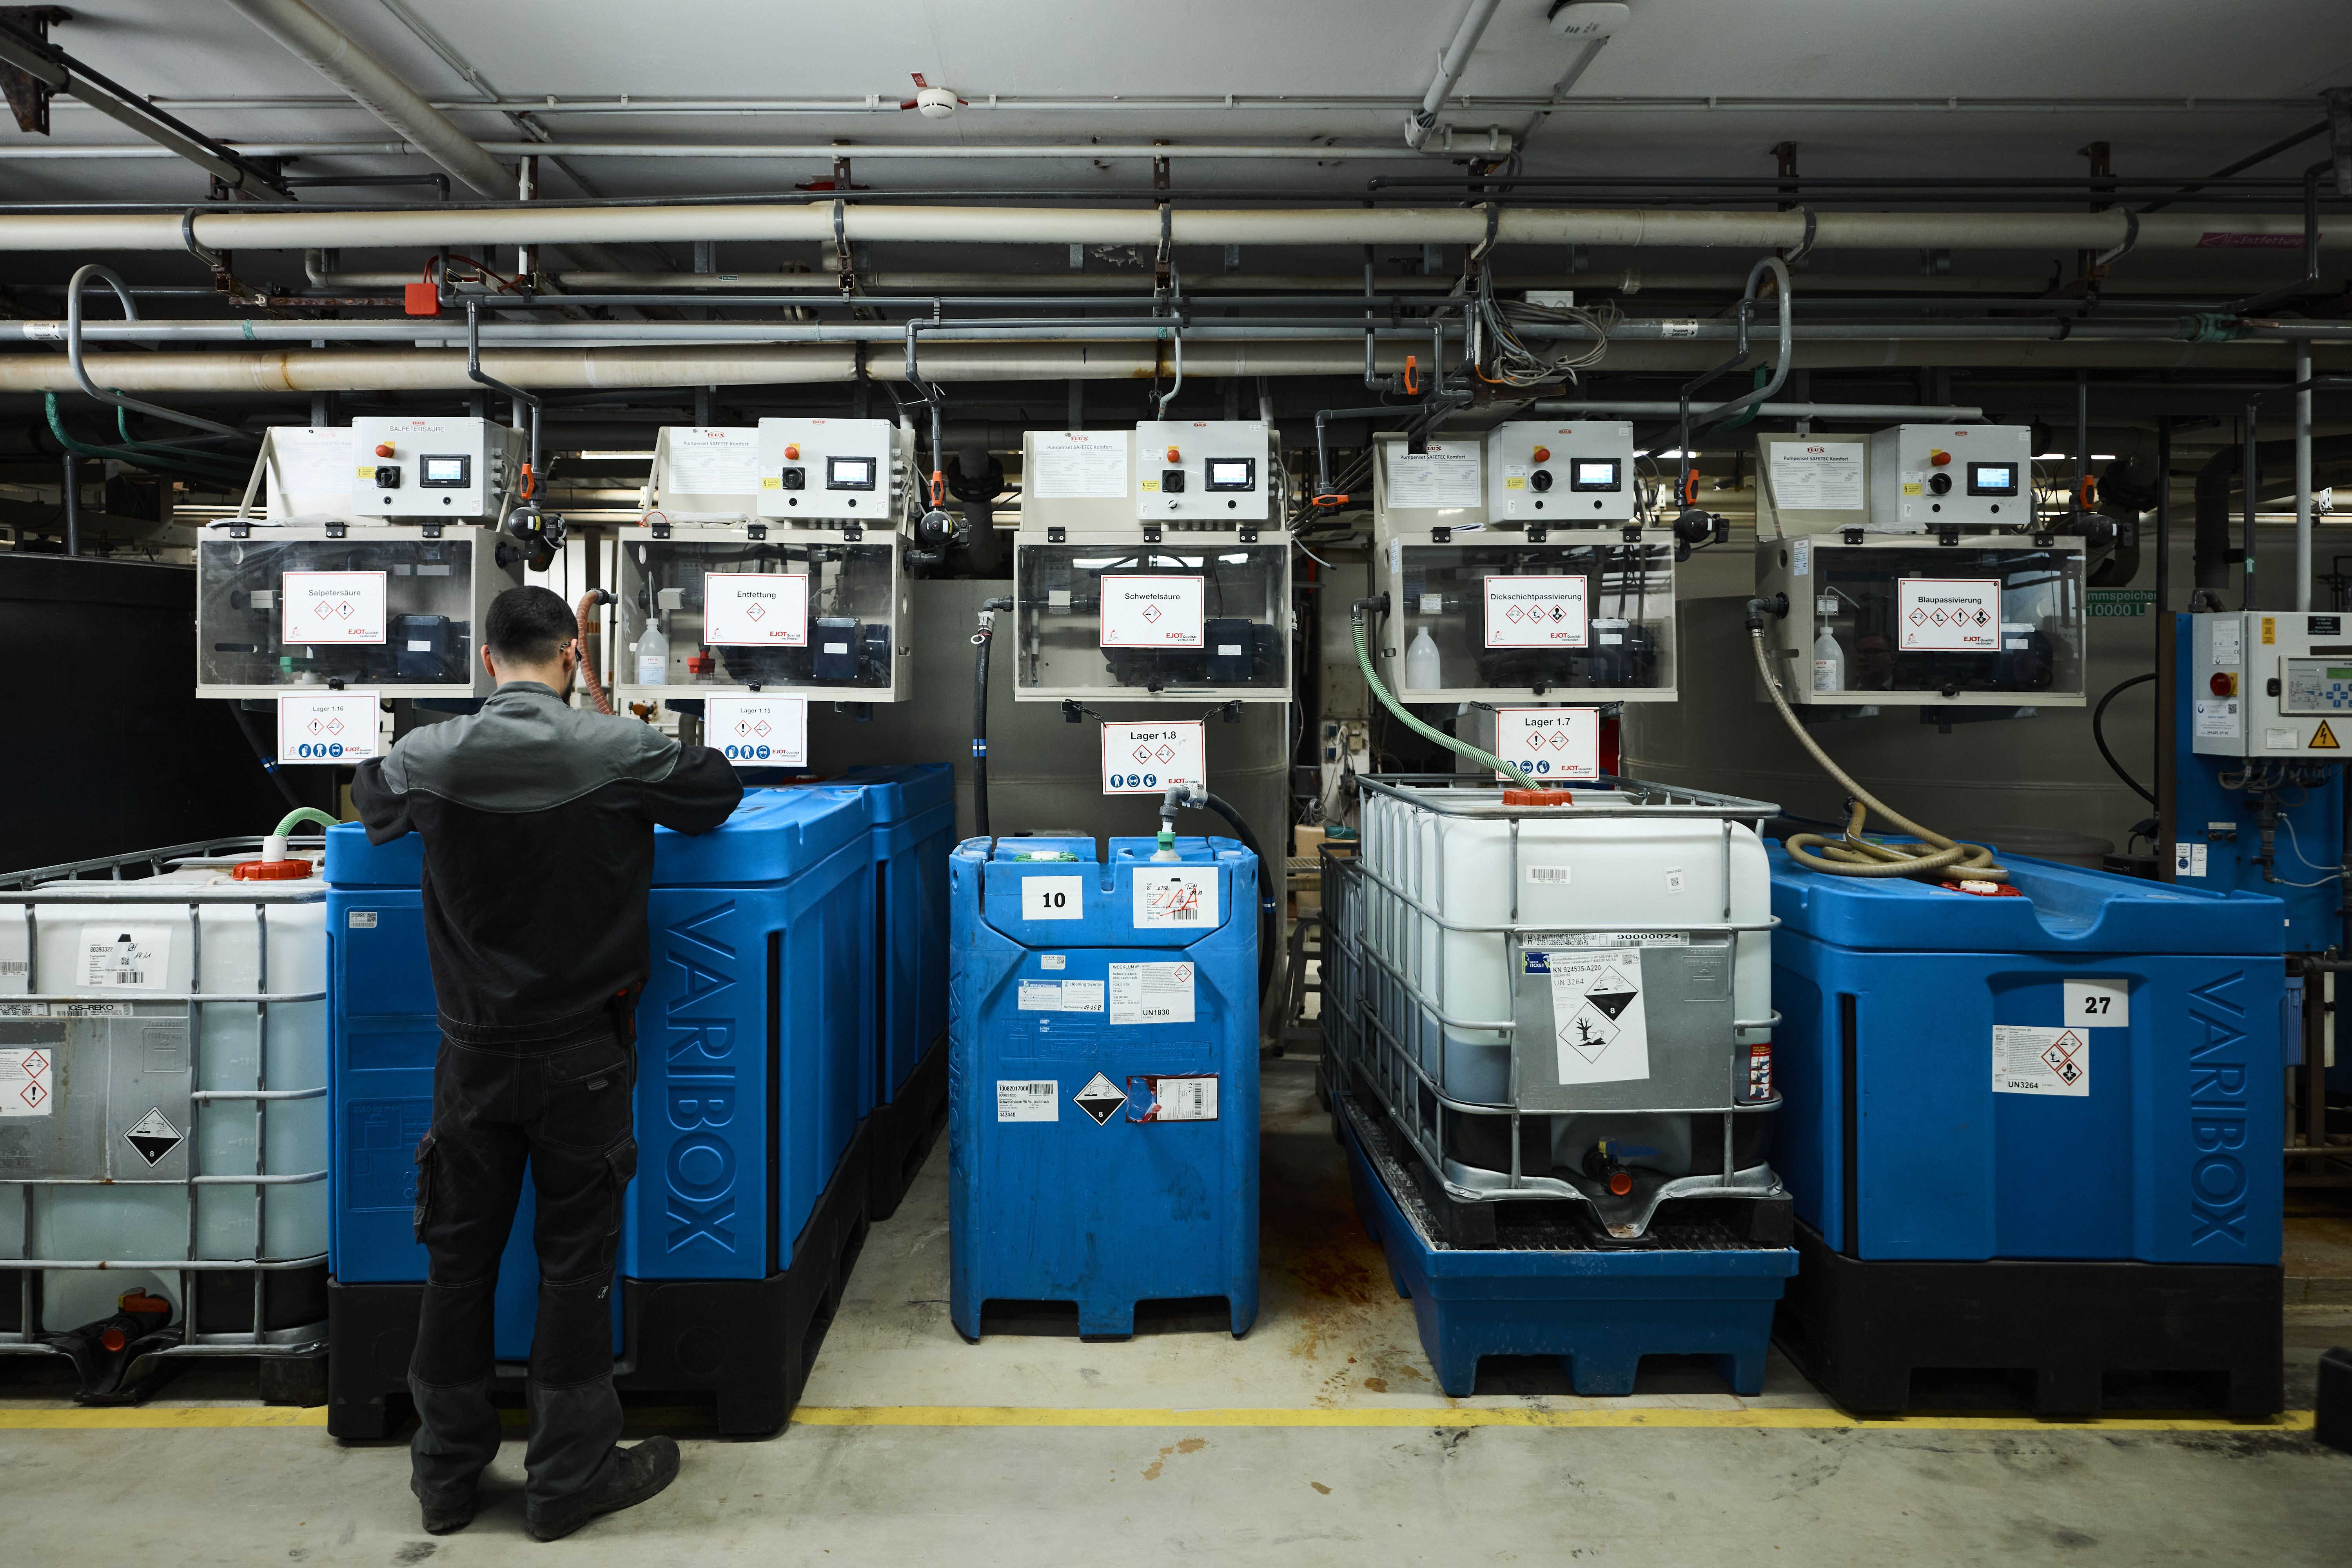
Specific application scenarios, suitable setups, and clear solutions—our application reports show how FLUX pumps are used in real-world applications.
Safely filling high-viscosity silicone oils at a delivery height of over 10 m
Refueling with Special Fuels Safely and Precisely
Automatic and virtually complete filling of industrial greases
Pumping Lime Milk from IBCs with Minimal Wear
Getriebe präzise mit Schmierfett befüllen – nahezu restlose Fassentleerung
Metallbearbeitungsöle aus gestapelten IBCs sicher abfüllen
Polituren effizient aus Mischkesseln abfüllen
Kühlschmierstoffe mischen und präzise abfüllen
Getriebeöl mengenpräzise dosieren mit halbautomatischem System
Certificates
Certified safety for a wide range of industries and countries: FLUX products are developed and certified for worldwide use and meet the highest requirements and safety standards. With FLUX, you’re always on the safe side, no matter where you are.

CE Conformity
All products comply with the EC Machinery Directive 2006/42/EC.

ATEX 2014/34/EU
Explosion protection in accordance with the ATEX Directive for potentially explosive atmospheres.
Product solutions for Chemical Applications
The following products are particularly well-suited for chemical applications. However, depending on the medium, process, and operating conditions, other solutions may be more appropriate. Please feel free to contact us for advice—we’ll help you select the optimal design.
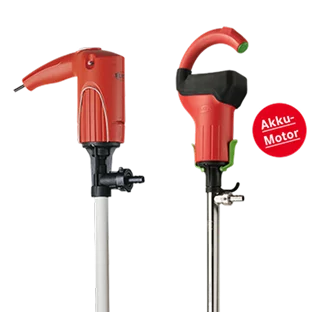
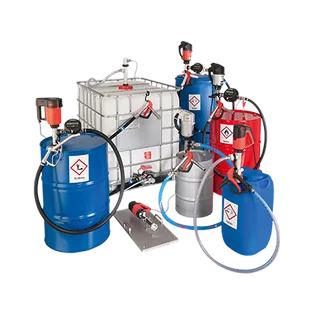
Series 300 Drum Pumps – JUNIORFLUX/COMBIFLUX
For smaller, low-viscosity fill volumes
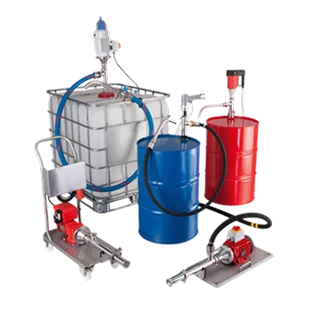
Series 400 Drum Pumps
For a wide variety of applications and low-viscosity fluids
Progressive cavity pumps VISCOPOWER
For low- to high-viscosity media in the industrial, pharmaceutical, food, and cosmetics sectors
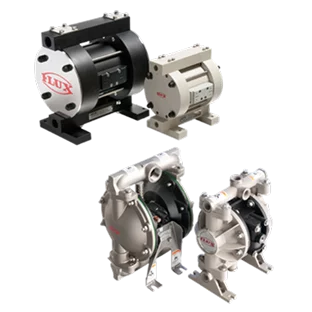
Air-operated diaphragm pumps
Self-priming pumps, including those designed for abrasive media, available in solid construction and in die-cast or cast versions
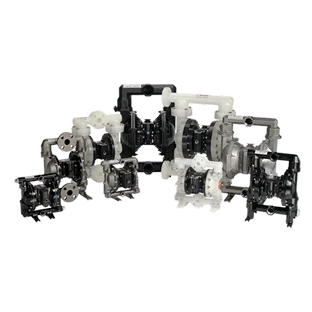
Double diaphragm pumps from ARO®
For pumping clean, low-viscosity fluids, as well as corrosive, abrasive fluids of medium viscosity and even coarser solids
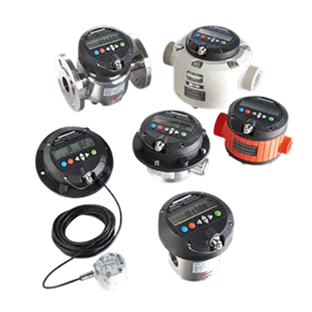
Flow meters
For manual or semi-automatic filling of a wide variety of fluids
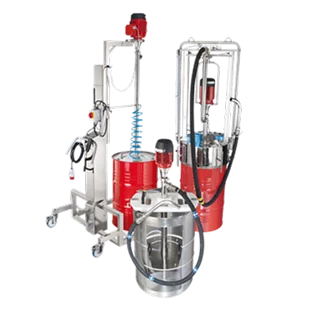
Drum emptying systems
For pumping high-viscosity fluids from a wide variety of drums
Get in touch.
Find documents.

Sales & Advice
Select a pump suitable for the application
We determine the medium, flow rate, viscosity and operating environment.

Requests for quotations
Please send us your requirements
We will assess your requirements and advise you on the most suitable option.

Service & Support
Documents for planning, operation and servicing
Find user manuals, dimension sheets, technical specifications and FAQs.